
Bandsaw Cutting Fluid: What We Run and How to Mix It
Coolant is the cheapest thing in the saw and it decides how long the most expensive consumable lasts. Run a blade dry, or in coolant that went off three weeks ago, and the teeth lose their edge in a fraction of the time. The first thing you usually notice isn't a slow cut. It's a crooked one.
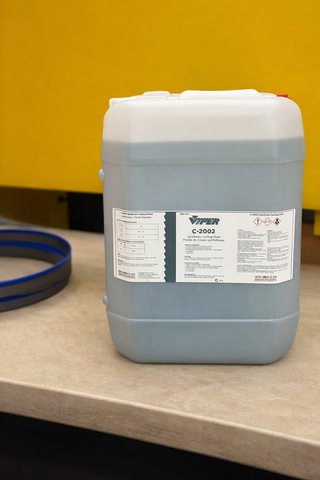
We stock two fluids, both made by Viper and both in 20 L jugs at our shop in Hamilton. C-2002 is a synthetic we run in flood systems, which covers most horizontal saws. CoolMist is a semi-synthetic for mist and jet setups. Work out your mix here, then read on for the things the label doesn't tell you.
How much concentrate does your tank need?
Put in the tank size and the kind of cutting you do. It works out the mix and how many 20 L jugs of C-2002 that takes.
Not on the plate? Measure inside the tank in centimetres: length × width × fill depth ÷ 1000 gives you litres.
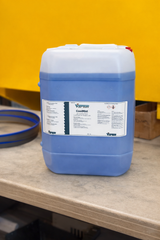
Running a mist or jet system? CoolMist is the semi-synthetic we sell for those. Same 20 L jug.
Synthetic or semi-synthetic
A synthetic like C-2002 has no mineral oil in it. It mixes clear, stays cleaner in the tank, holds up better against bacteria, and keeps rust off the saw and the parts. For a flood system on a horizontal saw cutting steel all day, that's what we put in.
A semi-synthetic carries some oil, which gives a little more lubricity right at the tooth. That's why CoolMist suits mist and jet systems, where you're putting a small amount of fluid straight at the cut instead of recirculating a tank of it.
Straight cutting oil has its place on the odd tough alloy job with a brush. It doesn't belong in a sump.
Mixing it right
- Concentrate into water, never the other way around. Run the water first and add the concentrate to it. Pour water into concentrate and you risk a mix that never properly comes together, especially with anything that has oil in it.
- Start at the ratio for the job. Around 1:10 for heavy cuts and stainless, 1:15 for general steel, 1:20 for light work. Too lean and the table and vise start rusting inside a week. Too rich wastes money and leaves a sticky film on everything.
- Check it. A refractometer takes ten seconds. Multiply the reading by the factor on the label and you know where you stand instead of guessing by colour.
- Top up with a weak mix. Water evaporates and the concentrate stays behind, so topping up with full-strength mix creeps the tank richer every week. Half strength is a good place to start; let the refractometer tell you from there.
When it's done
Coolant doesn't last forever, and a tank that's gone bad costs you blades, rusts parts and gives your operators rashes. Signs it's time:
- It smells. That rotten-egg smell on a Monday morning is bacteria that grew over the weekend.
- There's a layer of oil floating on top. That's tramp oil from hydraulic and way leaks, and it feeds the bacteria. Skim it off and fix the leak.
- Fresh cuts rust overnight, or the saw table does.
- It foams, or it's gone dark and murky.
When it's time, drain it, shovel the chips and sludge out of the bottom of the tank, clean the screen, rinse, and refill fresh. Skipping the clean-out is the most common mistake we see. The sludge in the bottom is where the bacteria live, and it will turn a fresh tank in a couple of weeks.
Getting it where it needs to go
The coolant has to land on both sides of the blade right where it enters the work. Coolant pouring onto the vise looks busy and does nothing. You want a steady flow at the cut, not a fire hose throwing chips around the shop.
Keep the chip brush working too. If the brush isn't clearing the gullets, chips ride back into the cut and no amount of coolant fixes that.
If the flow has dropped off and the lines are clear, the pump may be done. We stock a 115 V centrifugal coolant pump that suits most horizontal and vertical saws. Call with your saw model and we'll confirm it fits.
Ordering
Both fluids come in 20 L jugs. Add them to a blade order online, or pick them up at the shop on Bigwin Road in Hamilton. Running several saws and want to talk quantity? Call 1 (800) 957-2690.
Custom welded to your machine's exact loop length at our Hamilton, Ontario facility.
Configure & Order